Vacuum Conveying Solutions

Optimise Your Production Line with Piab Vacuum Conveying Systems

Upgrade from messy, inefficient mechanical conveyors. Move powders, granules, and delicate products safely and efficiently with an enclosed, hygienic, and ATEX-certified vacuum transfer system.

Speak to a Solution Specialist

Or call us today 1300 476 386

Safe. Closed. Efficient.

The Smart Way to Move Bulk Materials.

Stop losing product to dust, spills, and cross-contamination. Unlike traditional belts, screws, or bucket elevators, Piab vacuum conveying systems offer a completely enclosed powder transfer system. Whether you need to automate a manual process or optimise an existing line, we deliver solutions that protect your product and your people.

Industries

Food & Beverage

Hygienic, food-grade conveying for powders, sugar, flour, and coffee. FDA and EU compliant designs ensure no cross-contamination and rapid, easy cleaning between batches.

Pharmaceutical & Nutraceutical

Hygienic, food-grade conveying for powders, sugar, flour, and coffee. FDA and EU compliant designs ensure no cross-contamination and rapid, easy cleaning between batches.

Chemical & Industrial

Hygienic, food-grade conveying for powders, sugar, flour, and coffee. FDA and EU compliant designs ensure no cross-contamination and rapid, easy cleaning between batches.

Australia’s Trusted Pneumatic & Vacuum Solution Specialists.

Since 1987, Pneumatic Products has been helping Australian businesses optimise productivity, efficiency, and performance.

We go beyond simply supplying parts. We design, test, and deliver innovative pneumatic and vacuum solutions that actually work. We have built our reputation on authenticity, clear communication, and delivering long-term value to every client.

Talk with Our Experts

Face to face
Australia-wide support

Direct sales, support, and on-site solutions. Anywhere in Australia.

Complete End to End Solutions

We deliver the entire solution, taking your project from an initial quote to a fully operational system.

Backed by the global strength of Piab Group

Specialist vacuum-handling expertise backed by a global automation leader.

Discover the Piab piFLOW® Range

Innovative vacuum conveyors designed for every application, from heavy industrial bulk transfer to ultra-hygienic pharmaceutical manufacturing.
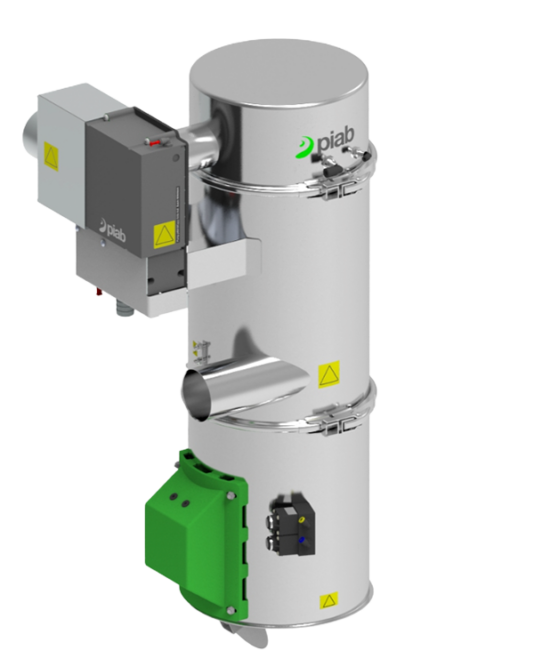
piFlow®i

ASTM 304 pickled surface.

Recommended for the additive, battery, chemical and general segments
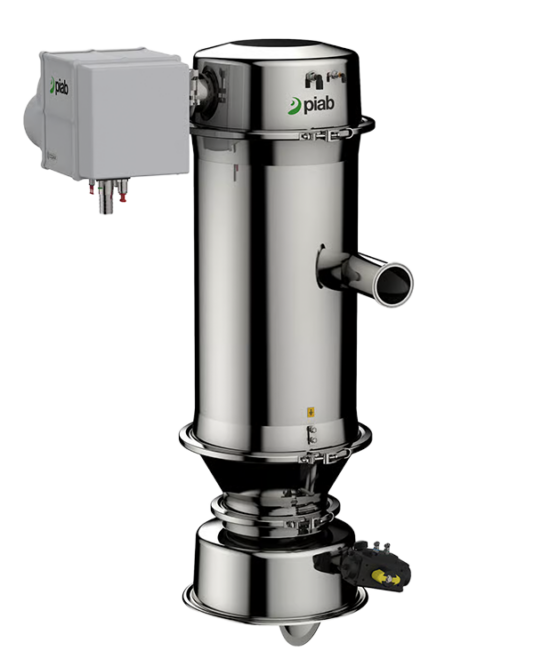
piFlow®p

ASTM 316 polished surface.

Recommended for all segments, especially food and pharmaceutical
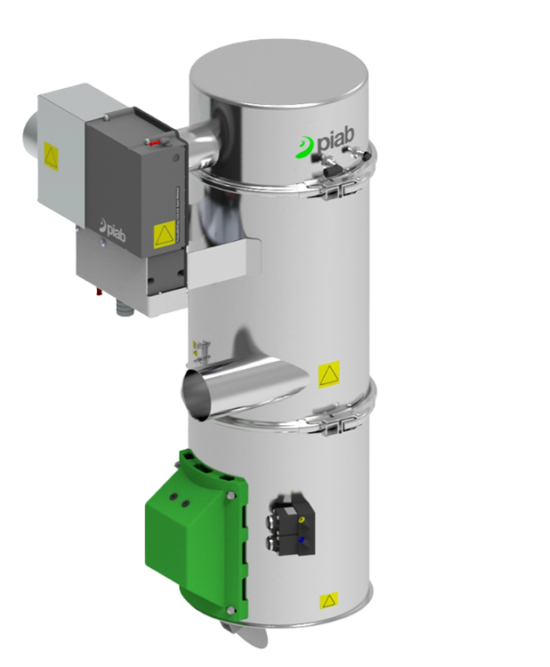
piFlow®f

ASTM 304 pickled surface.

Recommended for the food and nutraceutical segments
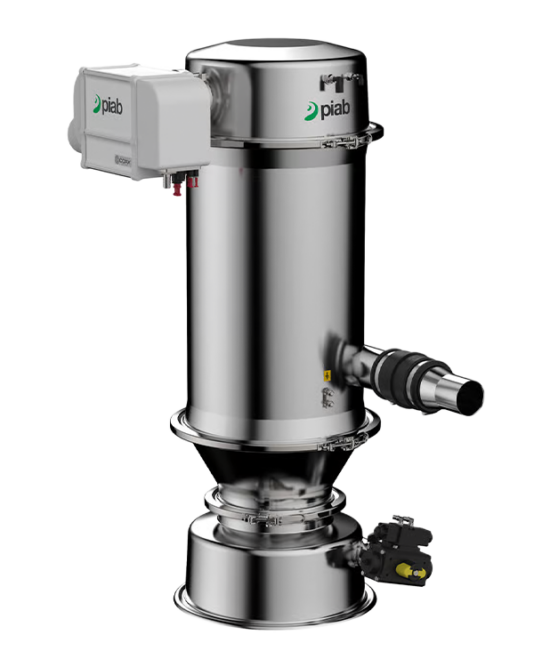
piFlow®fc

ASTM 304 electro-polished surface. 

Recommended for all segments, especially food and nutraceutical
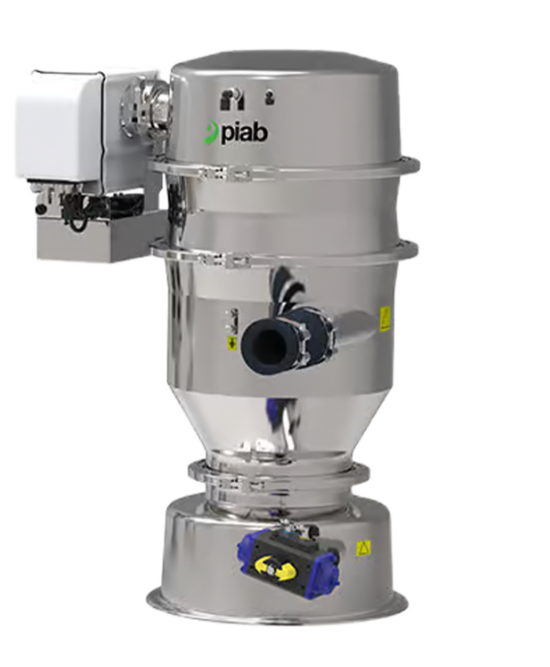
piFlow®t

ASTM 316 polished surface.

Recommended for segments with fragile products, especially nutraceutical and pharmaceutical
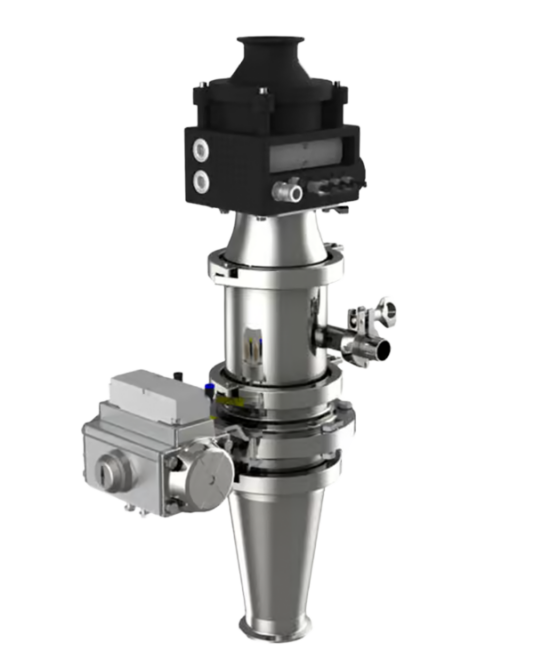
piFlow®am

ASTM 316 polished surface.

Recommended for additive manufacturing applications where space is limited

Recent Case Studies
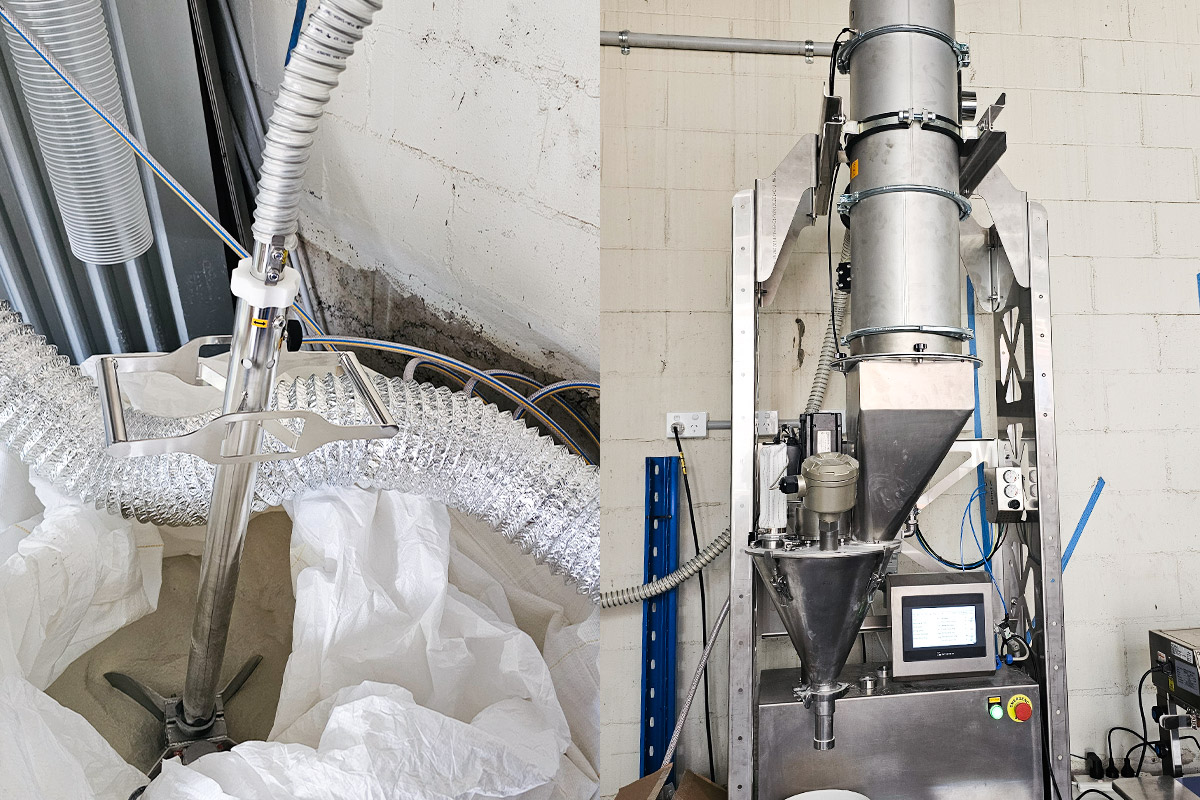
Piab piFLOW®i Vacuum Conveying Solves Zeolite Powder Transfer Challenge for Machine Technology

As Machine Technology’s zeolite product line grew, they identified a critical bottleneck: manually transferring zeolite powder from bulk bags...

Pharmaceutical and Nutraceutical Manufacturing with Piab Vacuum Conveying

In the fast-paced and highly regulated industries of pharmaceutical and nutraceutical manufacturing, maintaining efficiency and ensuring cost-effectiveness is crucial for success...

How to best convey tablets and capsules

The beauty of Piab’s vacuum conveying solutions lies in their adaptability. Our systems can be tailored to meet the specific needs of your production line...

Frequently Asked Questions

Unlike open belt conveyors, bucket elevators, or flexible screws that can cause spills, dust, and cross-contamination, vacuum conveying is a completely enclosed system. This protects your product from the environment and your staff from hazardous dust. Vacuum systems also have a much smaller physical footprint, fewer moving parts to maintain, and are significantly faster to clean.

No, not if you use the right technology. While standard conveying can be rough, the Piab piFLOW®t is specifically engineered for fragile goods. It uses an innovative, gentle conveying technology to transport tablets, capsules, and delicate food items smoothly, eliminating chipping, breaking, and batch segregation.

We do not guess. We test. We know that every powder, granule, and bulk material behaves differently. That is why Pneumatic Products offers comprehensive in-house testing. We test your specific material to understand its flow characteristics, allowing us to specify and guarantee the exact Piab solution needed for your production line.

Yes. Piab's industrial and premium vacuum conveyors are ATEX-certified. This means they are explicitly designed and approved to safely handle combustible dusts and operate in hazardous environments, effectively mitigating the risk of dust explosions in chemical, food, and pharmaceutical plants.

They are designed specifically for rapid changeovers. The entire piFLOW® range, especially the Food (piFLOW®f) and Pharma (piFLOW®p) models, features an intelligent quick-release design. The entire conveyor can be dismantled rapidly without tools for thorough cleaning and sanitation, ensuring you meet strict FDA and EU hygiene standards with minimal downtime.

Pneumatic Products specialises in face-to-face and onsite support, working directly with customers to understand their application and recommend the right solution. Our Sydney-based team provides local expertise with a friendly, family-driven approach, regularly travelling across Australia to support projects wherever they’re needed.

Ready to Optimise Your Automation System?

Speak with the Pneumatic Products team to find the right solution for your application - From standalone units to complete, automated powder transfer systems.
© 2026 Pneumatic Products Pty Ltd. All Rights Reserved.

piFlow®i

This is a conveyor widely used in the general industry and sometimes in the chemical industry. It has a high throughput performance as well as a small foot print. This conveyor is often used as an alternative to mechanical conveyors when there is a requirement for dust free conveying or low maintenance. Another advantage is that the pump is based on COAX® technology which is the most energy efficient way to produce vacuum. Capacity up to 7,5 tons/h.

Features

  • COAX® Technology is used in the pump. The most energy efficient way to produce vacuum.
  • The material used is ASTM 304.
  • piFLOW®i is easy to install and easy to use.
  • It is ATEX Dust certified.
  • It has antistatic filter and seals.
  • piFLOW®i is an cost-effective solution when no hygienic standards are needed, e.g. FDA.


piFlow®p

Our premium conveyors are designed with a Stainless Steel body (ASTM 316L) and meet the very high hygienic demands of FDA. Piab conveyors are ATEX Dust and Gas certified. Typical applications are powder and granules transfer or form-fill-seal or big bag loading and unloading drum/bag filling and emptyingor Mill/Sieve/Mixer/Blender filling or tablet/fragile products transfer or applications in explosive atmosphere or hygienic applications or compact applications.

Features

  • A premium steel grade vacuum conveyor, designed to meet the requirements of high-demanding applications for chemical, food and pharma industries.
  • Our COAX® Technology, the most energy efficient way to produce vacuum, is used in the pump.
  • Material in contact with the conveyed product is in compliance with FDA, EC No. 1935/2004 and EC No. 10/2011.
  • ATEX Dust, ATEX Dust and Gas certified.
  • Steel quality ASTM 316L (stainless steel, acid resistant), mechanically polished.
  • Designed according to USDA guidelines.
  • Antistatic filter and seals are available.
  • Automatic filter cleaning.
  • Hygenic design making maintenance and cleaning simple.
  • Wide capacity range from 2 to 56 liters per conveying cycle (up to 15 tons per hour).

piFlow®f

This conveyor is widely used in industries where food-grade quality and functionality are required. Typical applications include food-grade powder and granule transfer, feeding mills, sieves, mixers or blenders, gentle transfer of tablets and other fragile products, big bag loading and unloading, as well as installations operating in explosive atmospheres.

Features

  • An entry-level vacuum conveyor designed for industries where food grade quality, a dust free environment and easy maintenance are required.
  • Our COAX® Technology, the most energy efficient way to produce vacuum, is used in the pump.
  • Material in contact with the conveyed product is in compliance with FDA, EC No. 1935/2004 and EC No. 10/2011.
  • ATEX Dust certified.
  • Steel quality ASTM 304 (stainless steel), pickled surface treatment.
  • Antistatic filter and seals.
  • Automatic filter cleaning.

piFlow®fc

This is a conveyor widely used in the industry where food grade quality is a demand. Typical applications are: Food grade applications or powder and granules transfer or mill/sieve/mixer/blender filling or tablet/fragile transfer or big bag loading and unloading or applications in explosive atmosphere.

Features

  • Same heavy-duty design as the p- and t-series, targeting food and other industries not requiring acid resistant design of conveyors.
  • Our COAX® Technology, the most energy efficient way to produce vacuum, is used in the pump.
  • Material in contact with the conveyed product is in compliance with FDA, EC No. 1935/2004 and EC No. 10/2011.
  • Steel quality ASTM 304 (stainless steel), electropolished surface treatment.
  • Antistatic filter and seals are available.
  • Automatic filter cleaning.
  • Hygenic design making maintenance and cleaning simple.

piFlow®t

Perfect fit for transport of fragile materials, where the unique piGENTLE® functionality secures a smooth and stable product flow.

Features

  • Perfect fit for transport of fragile materials, where the unique piGENTLE® functionality secures a smooth and stable product flow.
  • Our COAX® Technology, the most energy efficient way to produce vacuum, is used in the pump.
  • Material in contact with the conveyed product is in compliance with FDA, EC No. 1935/2004 and EC No. 10/2011.
  • ATEX Dust, ATEX Dust and Gas certified.
  • Steel quality ASTM 316L (stainless steel, acid resistant), mechanically polished.
  • Designed according to USDA guidelines.
  • Antistatic filter and seals are available.
  • Automatic filter cleaning.
  • Hygenic design making maintenance and cleaning simple.
  • Deduster function with pre-separator solution.

piFlow®am

Specifically developed for additive manufacturing applications are designed with a stainless-steel body (ASTM 316L) and a butterfly valve. These conveyors have a standard TC-coupling for easy integration and designed to take up minimal amount of space. Typical applications are metal powder transfer to or from a hopper or a sieve, feeding a 3D printer or recirculating material from the overflow bin.

Features

  • A premium steel grade vacuum conveyor, designed to meet the requirements of high-demanding applications in additive manufacturing and pharma industries.
  • Our COAX® Technology, the most energy efficient way to produce vacuum, is used in the pump.
  • Material in contact with the conveyed product is in compliance with FDA
  • Conveyor is CE approved
  • Steel quality ASTM 316L (stainless steel, acid resistant), mechanically polished.
  • Designed according to USDA guidelines.
  • Automatic filter cleaning.
  • Hygienic design making maintenance and cleaning simple.
  • 0.5 liters per conveying cycle